addlinkspot
  • Home
  • Resources
  • Frontend
  • Guide
  • Backend
Business

Water Play Structure Spare Parts and Service Life Planning

by addlinkspot November 22, 2026
written by addlinkspot

The lifespan of an aquatic attraction is shaped by hundreds of small decisions made after installation, from the way connections are inspected to how replacement components are sourced. A durable water play structure still requires regular care because constant moisture, water chemistry, sunlight, and repeated mechanical movement gradually affect different materials in different ways.


Facilities that plan for component replacement before faults occur can make maintenance more predictable and avoid unnecessary closures. Jinchao supplies customized aquatic play solutions, making equipment configuration and long-term maintenance relevant considerations during project planning.


Understanding Component Wear and Replacement Cycles

Not every part of an aquatic attraction deteriorates at the same rate. Water nozzles may become restricted by mineral deposits, seals can lose flexibility, and moving joints may develop looseness through repeated use. Structural fasteners face different stresses from decorative panels, while exposed surfaces may be affected by ultraviolet radiation or cleaning agents. Treating the entire attraction as a single maintenance unit can obscure these differences and make inspections less effective.


Material performance depends on both its properties and its operating environment. Hot-dip galvanized steel uses a protective zinc coating to help limit corrosion, but damaged coatings and persistent moisture can still require attention. Fiberglass can provide a durable slide surface, although impact damage, surface wear, and unsuitable cleaning methods may shorten its useful life. Stainless steel grades also vary in their resistance to corrosion, particularly where water chemistry or cleaning practices are poorly controlled. Inspection plans should reflect the actual materials used rather than assume every component needs the same treatment.


Usage patterns provide another clue to expected service life. An attraction operating throughout a busy summer season may experience more mechanical cycles and cleaning than one used occasionally at a hotel pool. Maintenance records should capture inspection dates, faults, adjustments, repairs, and replacement history. Over time, these records help identify recurring problems and establish realistic inspection intervals based on evidence rather than arbitrary calendar reminders.


Organizing Spare Parts and Procurement

A useful spare-parts inventory prioritizes components according to safety significance, failure likelihood, replacement difficulty, and delivery time. Small seals or standard fittings may be inexpensive and easy to source, while a custom fiberglass section or specialized rotating assembly could require a longer manufacturing period. Holding every possible spare is rarely practical; maintaining critical items that could otherwise cause prolonged downtime is often a more effective approach.


Accurate identification is essential before replacement orders are placed. Part references, dimensions, material grades, connection types, technical drawings, and photographs help distinguish components that may look similar but serve different purposes. Unverified substitutes can create problems with fit, corrosion resistance, mechanical performance, or structural compatibility. Safety-critical parts should be replaced only according to manufacturer instructions and, where necessary, assessed by qualified technicians.


Facilities using splash pads should also consider the relationship between individual components and the wider water-delivery system. A blocked spray nozzle may affect one play feature, whereas a failed valve or circulation component could interrupt several areas at once. The inventory should identify which parts can be replaced locally, which require specialist support, and which need to be ordered from the original supplier. Operators comparing water play equipment providers can ask about spare-part availability, technical documentation, warranty conditions, and the process for diagnosing faults after installation.


Storage conditions deserve attention as well. Rubber seals can deteriorate under unsuitable temperatures, metal components may corrode in damp environments, and fiberglass parts can suffer damage if stacked or handled incorrectly. Each stored item should be labeled, protected, and recorded so staff can locate it quickly. Periodic inventory reviews also prevent obsolete or expired components from remaining on the shelf unnoticed.


Extending Service Life Through Planned Maintenance

A preventive maintenance program should connect daily observations with scheduled technical inspections. Frontline staff can watch for leaks, unusual noises, loose fittings, rough surfaces, and inconsistent water flow, while qualified maintenance personnel carry out more detailed checks of structural connections, moving mechanisms, and safety-related components. Clear reporting procedures matter because a small irregularity may become a larger fault if it is repeatedly ignored.


Cleaning practices should match the materials and the water conditions. Mineral deposits may require suitable descaling procedures, but aggressive chemicals can damage protective coatings, seals, and surface finishes. Water chemistry should be monitored in line with the facility’s operating requirements, and any maintenance involving electrical, mechanical, or structural systems should follow appropriate isolation and safety procedures. Repairs should be documented, including the parts used and any follow-up inspection required.


Seasonal closures offer a useful window for maintenance that is difficult to perform during public operation. Teams can inspect concealed connections, examine exposed steelwork, test moving features, and check slide surfaces before reopening. Facilities in freezing climates may also need to drain or protect water-bearing components according to manufacturer guidance. A documented pre-opening inspection helps confirm that repairs have been carried out and that the attraction is suitable for operation.


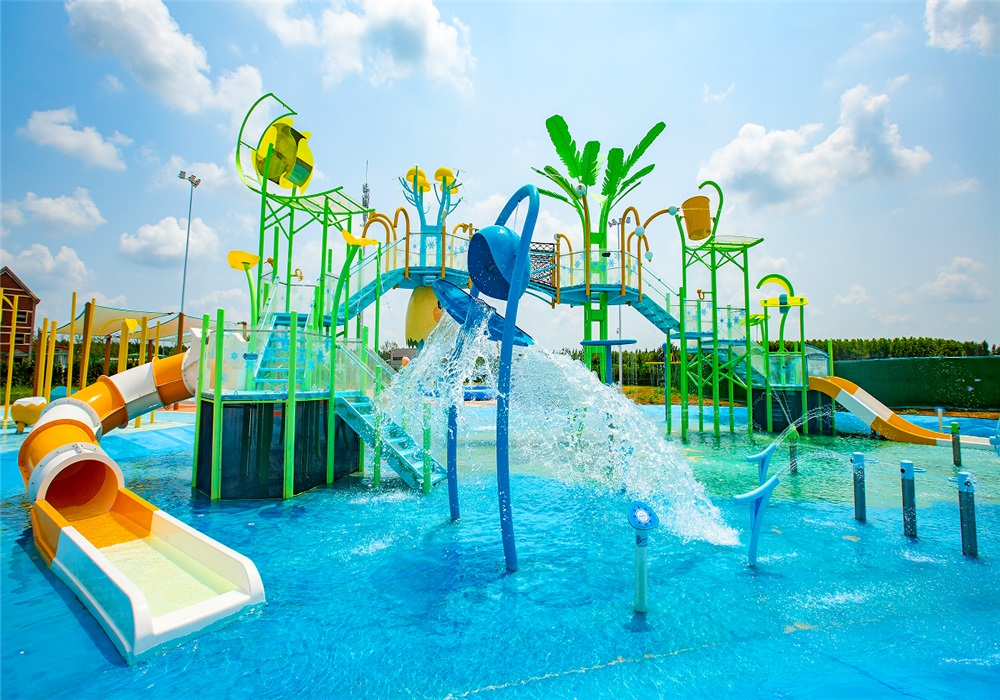
The design itself can affect how easily future maintenance is performed. Jinchao’s Small Water House is intended for settings such as amusement parks and hotel swimming pools, with a suggested pool area of approximately 200–500 square units. Its specified materials combine hot-dip galvanized steel with fiberglass slides, and the theme can be customized for the project. For this configuration, service planning should account for coating condition, structural joints, slide surfaces, water outlets, and the accessibility of components that may need periodic inspection or replacement.


Conclusion

Long-term upkeep becomes more manageable when component records, procurement decisions, and inspection routines work together. A maintenance team needs more than a checklist: it needs accurate equipment references, clear fault-reporting procedures, and a realistic understanding of which failures require immediate shutdown. Those foundations allow operators to respond to wear before it causes avoidable disruption.


Before each operating season, facilities should review repair history, verify the availability of critical spare parts, and reassess inspection intervals against actual usage. Any damage that could affect structural integrity or visitor safety should be evaluated by qualified personnel before the affected attraction returns to service.


With customization and maintenance requirements considered early, Jinchao can be assessed as a supplier for water play structure projects where operational longevity matters alongside initial design. Thoughtful planning helps facilities manage repair costs, shorten avoidable downtime, and maintain a more reliable aquatic play environment.
November 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

How Can Dispensing Process Data Improve Production Traceability?

by addlinkspot November 22, 2026
written by addlinkspot

Production traceability becomes more reliable when every dispensing cycle can be connected to recorded process conditions, material details, and inspection results. A precision dispensing system can contribute to this record by capturing relevant operating parameters, helping manufacturers investigate defects, compare production batches, and identify deviations before they affect more units. Axxonauto operates in industrial dispensing and coating, fields where process documentation can support quality management across increasingly automated manufacturing environments.


How to Connect Each Dispensing Cycle to a Verifiable Record?

A useful traceability record goes beyond a timestamp or machine identification number. Depending on the application, it may include the workpiece serial number, material batch, recipe version, dispensing pressure, valve timing, temperature, and equipment status. Linking these details creates a history that helps quality teams understand the conditions under which a component was processed.


Material tracking is especially important for adhesives with limited working lives or specific storage requirements. Recording batch numbers, expiration dates, and material changeover times can help determine whether a quality issue is associated with a particular supply lot or handling event. This information becomes more valuable when the same material is used across several production lines.


Data also needs a clear relationship with the finished product. A machine log that cannot be matched to an individual workpiece or identifiable batch offers limited value during a recall or customer investigation. Barcode scanning, RFID identification, or integration with manufacturing execution systems can connect process records to the relevant product history.


Traceability element What to record Purpose
Workpiece ID Serial or batch number Link record to product
Material batch Lot and expiry Investigate material-related defects
Process parameters Pressure, temperature, valve timing Compare accepted and rejected units


How to Turn Process Measurements Into Actionable Evidence?

Raw measurements are useful only when their meaning is understood. In adhesive dispensing, recorded pressure, flow, valve timing, and movement data can help explain changes in bead width, deposit volume, or placement accuracy. Comparing these measurements with an approved process window allows engineers to distinguish normal variation from conditions that warrant investigation.


A practical monitoring plan should define which parameters matter most to product quality. For one application, deposit weight may be the most meaningful indicator; another may depend on bead continuity, temperature, or the position of each deposit. Collecting every available signal can create excessive noise, so measurement selection should follow the actual failure modes and acceptance criteria.


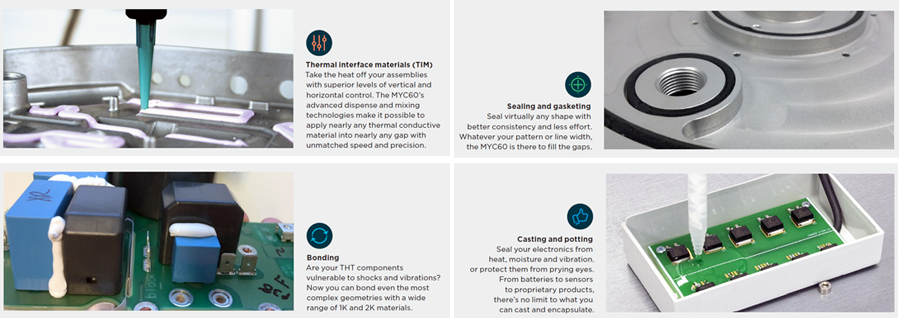
The MYC60 provides a useful example of equipment specifications that can form part of an application record. This industrial dispensing platform supports high-volume processing of many one-component and two-component materials, with inline or batch configurations and options for conveyor, trolley, and robotic integration. Its Z-axis travel of 120 mm and maximum top clearance of 230 mm define the vertical working envelope—two figures engineers can document when checking whether the intended workpiece and tooling fit within the available operating space, and whether the programmed dispensing path remains accessible across the full range of component heights.


How to Improve Defect Investigation and Batch Comparisons?

A traceable process makes it easier to narrow the scope of a defect investigation. If several rejected components share a material batch, recipe revision, or period of unstable pressure, engineers can test those relationships instead of inspecting every possible cause. Historical records also help determine whether a deviation is isolated or has appeared repeatedly.


Comparisons between accepted and rejected units can reveal patterns that visual inspection alone may miss. For example, a gradual change in dispensing pressure may coincide with nozzle wear, a partial blockage, or a material condition change. Such a correlation does not prove causation, but it gives technicians a focused starting point for physical inspection and controlled testing.


Effective records should preserve both the original measurements and any subsequent adjustments. If a technician changes a recipe to address an irregular deposit, the system should record who made the change, when it occurred, and which version was active during each production run. This history supports audits and helps prevent an unverified adjustment from becoming the default setting.


How to Establish Reliable Data Governance Across Production?

Traceability depends on consistent data definitions and reliable system clocks. If different machines use inconsistent parameter names, units, or time settings, comparing records across production lines becomes difficult. Standardized naming conventions, synchronized timestamps, and documented data formats help preserve meaning as information moves between equipment and factory software.


Access controls are equally important. Operators may need permission to run approved recipes, while process engineers may be authorized to revise settings under a controlled approval procedure. Version histories and audit trails can show whether a change was authorized and help distinguish routine production activity from unplanned intervention.


Data retention should reflect product risk, customer agreements, and applicable regulatory requirements. Records must remain readable and retrievable for the required period, with backups and access protections suited to their importance. A traceability system is most useful when teams can retrieve relevant evidence promptly without relying on personal spreadsheets or undocumented workarounds.


Conclusion

Production traceability improves when dispensing measurements, material identities, machine settings, and inspection outcomes form a connected history. The resulting records help manufacturers investigate defects, assess process stability, support audits, and make evidence-based decisions about corrective action. Data collection alone, however, cannot replace validated procedures or competent engineering judgment.


A well-integrated precision dispensing system can make process information easier to associate with individual products and production batches. Axxonauto is one source of industrial dispensing and coating technology that manufacturers may evaluate when reviewing equipment and data-integration needs, with the final configuration determined by application requirements and factory systems.


FAQs

Which Dispensing Parameters Should Be Recorded for Traceability?

Relevant parameters may include material batch and expiration details, recipe version, pressure, valve timing, temperature, deposit measurements, equipment status, and inspection outcomes. The appropriate set depends on the material, product design, and risks associated with dispensing defects.


How Does Process Data Help Identify the Cause of Adhesive Defects?

Engineers can compare records from accepted and rejected parts to find recurring differences in operating conditions, material batches, or recipe versions. These patterns help narrow the investigation, although physical inspection and controlled testing are still needed to confirm the cause.


How Can Manufacturers Evaluate Equipment for Traceability Requirements?

They should examine available data outputs, record granularity, recipe history, integration options, access controls, and data-retention capabilities. Axxonauto can be included in supplier research, with capabilities verified against the factory’s specific traceability and quality requirements.


November 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

Portable Multi Gas Detectors: How Channels Share One Pump

by addlinkspot November 20, 2026
written by addlinkspot

One sampling tube enters a portable gas detector, yet the screen can show several gas values in different units. The pump supplies a moving air sample, and each installed sensor measures its assigned gas or gas group. The number of channels reflects how many measurements the instrument can make from the sample delivered through that inlet.


Following the air through the instrument explains two features of a shared pump. All of the channels depend on delivery of a usable sample, while the units and response times belong to the individual measurements. The first question is when air from the current sampling point reaches the instrument.


What the Shared Pump Delivers


With the probe held away from the instrument, a length of tubing separates the air of interest from the sensing elements. The pump creates the flow that carries that air to the inlet of the portable gas detector. Until air from the probe arrives, displayed readings may still reflect air that was previously in the line.


One reason sharing the sampling hardware can make multi gas detectors portable is that each channel can use the same probe. A technician can carry one instrument and place one inlet at the location under observation. The tubing and any specified filter belong to the common delivery path, so their condition matters to every channel in use.


Once air arrives, the sensor configuration determines what can be measured. A channel fitted for oxygen produces an oxygen reading, while another sensor responds to the gas or gas group specified for that channel. A single inlet can support these separate measurements regardless of how a particular instrument routes gas between its internal sensing elements.


Why Readings Settle at Different Times


Oxygen reported as a volume percentage, carbon monoxide reported in parts per million, and combustible gas reported in %LEL can all describe the same sample. Their units follow the measurement assigned to each channel. A changing oxygen value and a changing combustible value can appear together without giving the same information about the air.


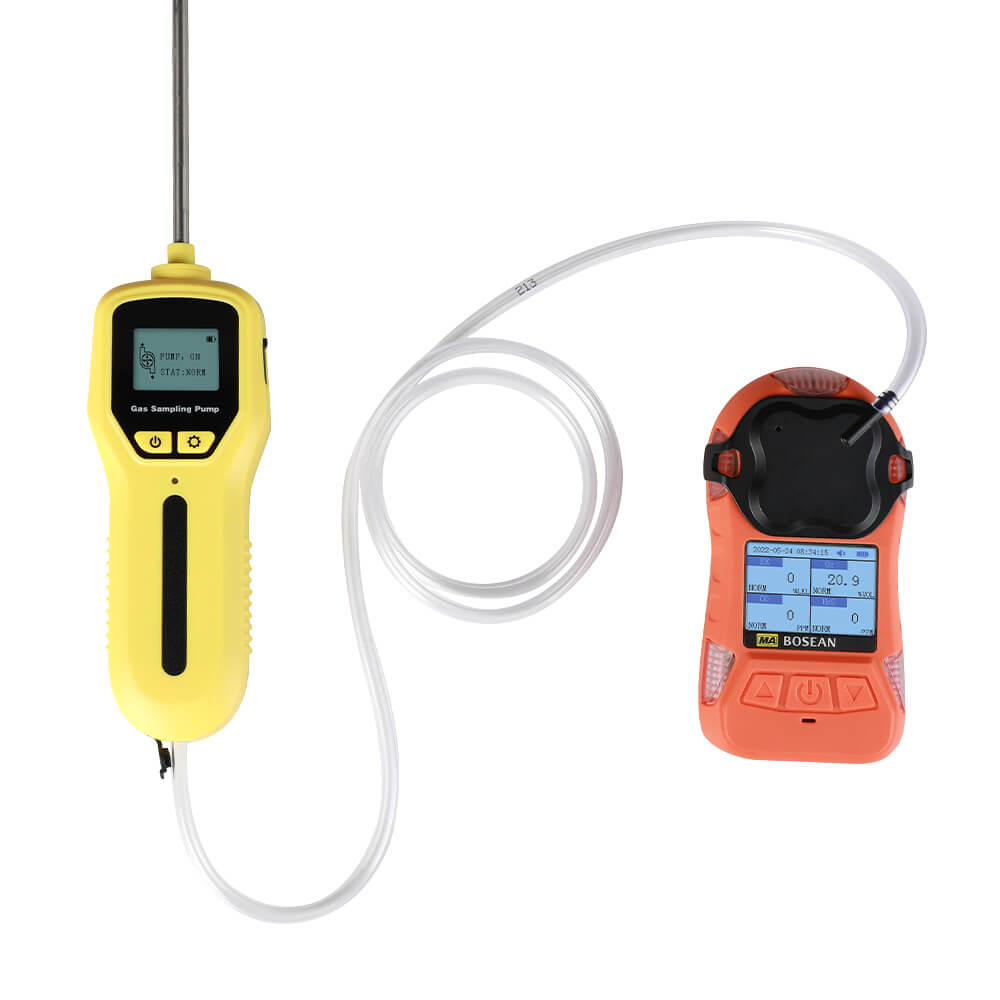
Six selectable flow settings on the Bosean K-600M cover 300–800 mL/min, and the instrument can read up to six configured gas channels at once. An integrated sampling pump is one way to keep multi gas detectors portable while giving the operator a choice of flow settings for an approved sampling arrangement.


Time in the sample line depends on the tubing dimensions and the actual flow through it. The line material must also be suitable for the target gas, and filter condition can affect delivery. Once new air reaches the instrument, the fitted sensors still need time to respond, so readings on the same screen can settle at different times.


At an actual flow of 300 mL/min, the pump would move a volume of air equal to the tube’s 150 mL internal volume in about 30 seconds. That calculation estimates transit through the tube alone. The interval needed for a measurement also depends on how the air mixes in the line and how each sensor responds.


Read a Pump Fault Separately From a Gas Alarm


If the pump fault warning appears on a portable gas detector, sample delivery needs attention even when the screen still shows gas values. A gas alarm refers to a reading on a configured channel. The pump fault warning on the Bosean K-600M concerns the shared sampling mechanism that the readings depend on.


Several readings can therefore be affected by one problem in the inlet path. Restricted flow through a tube or filter can delay air arriving from the probe, even when the sensors remain responsive. The installed line and filter are part of the sampling setup to be checked before readings from a new point are interpreted.


Numerical values and concentration curves offer different views of the same measurements. A K-600M record can be triggered by an alarm, captured at an interval, or saved manually to a TF card. After USB export, the record can be compared with the time a filter was changed or a probe moved to put the change in readings in context.


When a Separate Pump Serves the Same Purpose


An existing diffusion instrument can sometimes be used for pumped sampling if a compatible accessory is available. The Bosean ZC-600 is a separate self-priming diaphragm pump rated above 500 mL/min. Its arrangement delivers sample gas to a compatible instrument through a calibration cover fitted to that detector.


Keeping multi gas detectors portable with an external assembly involves carrying the detector and its sampling accessories as separate pieces. A built-in pump makes the instrument and its sampling mechanism a single unit. In either arrangement, the specified tubing, fittings, and operating conditions determine whether the instrument can receive a usable sample at the intended point.


A timing check belongs to the assembled equipment. If a crew changes from an integrated unit to an external pump with a calibration cover, the earlier estimate needs to be checked against the volume and flow of that setup. The readings can be interpreted together once the sample has arrived, the fitted sensors match the gases of interest, and the values have stabilized.


SEO Title: Portable Multi Gas Detectors: Shared Pump Sampling


Meta Description: See how a shared pump delivers samples to multiple sensors, why readings stabilize at different times and how a pump fault differs from a gas alarm.


November 20, 2026 0 comments
0 FacebookTwitterPinterestEmail
News

Quality Tests Used by Car Starting Battery Manufacturers

by addlinkspot November 17, 2026
written by addlinkspot

Starting batteries face demanding conditions long before a driver turns the ignition key. Cold mornings, repeated engine starts, vibration, and irregular charging can expose weaknesses that remain hidden during a simple voltage check. Manufacturers therefore need several types of quality tests, not just one final inspection.

For buyers sourcing an automotive starting battery, test methods matter as much as advertised specifications. Understanding what each assessment measures helps distributors, vehicle manufacturers, and fleet procurement teams compare products and request useful evidence before placing orders.


Cranking Tests Reveal Starting Capability

Cold cranking amps, or CCA, describe starting-current capability under defined test conditions. A laboratory uses a specified temperature, discharge procedure, and voltage threshold according to the selected standard. Purchasing teams should confirm which standard applies before comparing CCA figures from different suppliers.

The initial voltage reading cannot demonstrate whether a battery can deliver sufficient current during engine cranking. Load testing examines voltage behavior while current is drawn. Engineers also inspect the voltage recovery pattern after discharge to understand how the battery responds to demanding starts.

For a sodium ion batteries manufacturer, repeated starting tests add another layer. Testers apply controlled starting pulses with defined rest periods. They track voltage drop and temperature across cycles. These results help buyers assess batteries intended for taxis, delivery vans, or frequent restarts.


What Happens During Temperature Testing?

Battery output changes with temperature. Low-temperature testing examines starting performance after the battery has reached a defined cold condition. Test reports should identify the conditioning period, test temperature, discharge current, and pass criteria rather than presenting a cold-weather claim without context.

High-temperature evaluation investigates behavior during prolonged heat exposure. Engineers may monitor voltage, capacity retention, enclosure condition, and protection-system responses. A published operating-temperature range should not be confused with proof that every performance rating stays unchanged throughout that range.

Thermal cycling provides different information. Alternating cold and hot conditions can reveal problems with seals, connections, and mechanical components. For distributors serving several climates, these tests support product selection and reduce uncertainty about operation.


Durability Depends on More Than Cycle Count

Cycle-life testing repeats defined charge and discharge patterns until a specified endpoint is reached. Depth of discharge, temperature, current, and charging method strongly affect the outcome. Buyers should request the complete test conditions when reviewing claims about service life or start-stop endurance.

Vibration tests address a separate risk. Road movement can stress internal connections, terminals, and the battery case. A test fixture applies controlled vibration, followed by electrical and visual inspection. The selected vibration profile should reflect the intended vehicle application rather than an unrelated laboratory setting.

Charging compatibility deserves attention too. A replacement battery must work with the vehicle’s charging system and electrical requirements. Engineers examine voltage limits, charging response, and protective behavior. Matching case dimensions alone does not establish that a sodium-ion product can replace a conventional lead-acid unit.


Safety Checks and Production Consistency

Safety evaluation can include overcharge, short-circuit, and abnormal-temperature procedures selected for the battery chemistry and application. Results should record protection responses, physical changes, and test conditions. Buyers should distinguish between a test method proposed for qualification and evidence that a particular model has passed it.

Incoming material checks and production inspections complement laboratory qualification. Manufacturers can inspect component dimensions, electrical connections, assembly quality, and identification labels. Batch records also help trace components and investigate unexpected variations discovered during incoming inspection at a customer’s facility.

For bulk orders, consistency is especially important. Sampling plans should state how many units are tested, how they are selected, and which acceptance limits apply. Distributors can then compare shipments against an agreed quality specification instead of relying only on a single demonstration sample.


Product Specifications Need Verifiable Evidence

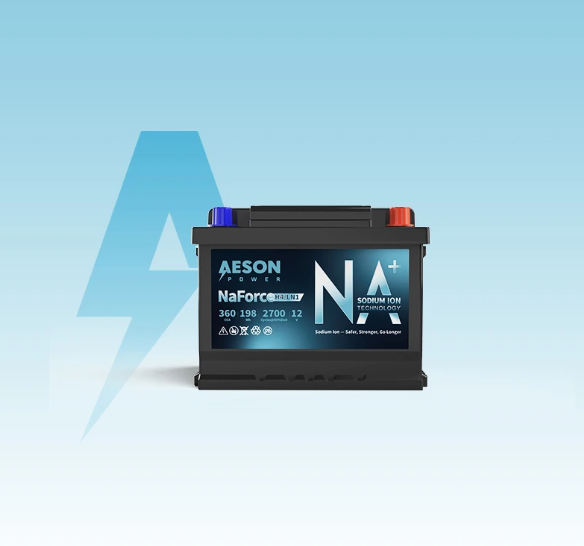
The H4/LN1 sodium-ion model listed by Aeson Power provides a useful example of specification review. Its published values are 12V, 360A CCA, and 198Wh. The listed weight is 3.5kg, with dimensions of 207 × 175 × 190mm. These figures establish a reference for product comparison, but do not replace independent application testing.

A buyer reviewing an automotive starting battery should request supporting test reports for its cranking output and temperature behavior. The report should identify the tested model, sample quantity, method, and measured results. Installation checks should also cover terminal layout, case fit, and electrical compatibility.

When assessing a sodium ion batteries manufacturer, procurement teams can ask whether test records are linked to production batches. Clear documentation helps connect design specifications, sample approval, and delivered units. It also supports technical discussions when customers report performance differences in service.


A Practical Checklist Before Procurement

Test documentation works better when purchasers define requirements early. Vehicle voltage, required cranking current, ambient temperature, duty cycle, and available installation space should form part of the inquiry. The supplier can then identify suitable products and explain which evaluations are relevant.

Quality agreements should specify inspection criteria, sample approval procedures, traceability, and handling of nonconforming units. A sodium ion batteries manufacturer should also clarify which test reports are available for the requested model and whether additional application validation is needed.

Aeson Power is an Australian battery company offering sodium-ion solutions for vehicle starting and related applications. They can discuss product specifications and sourcing requirements with commercial customers seeking to assess sodium-ion technology for their markets.

For the next automotive starting battery project, request model-specific test evidence and confirm vehicle compatibility before approving a bulk order.


November 17, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

What Are the Best Uses for Long Range Active RFID Tags in Modern Warehouse Management?

by addlinkspot November 13, 2026
written by addlinkspot

Warehouse management involves more than recording goods when they enter or leave a facility. Staff must locate pallets, track assets between storage areas, monitor equipment movement, and maintain accurate inventory records. These tasks become harder when warehouses cover large areas or handle frequent transfers. Radio frequency identification (RFID) can help businesses collect identification data without relying on manual barcode scans at every checkpoint.

The value of an RFID system depends on the type of goods, the layout of the facility, and the distance between tags and readers. Active systems are worth considering when assets move across wide spaces or require identification from a greater distance. Understanding their practical uses helps warehouse operators decide where this technology fits into their existing workflows.


Tracking Pallets Across Large Storage Areas

Pallets often move between receiving docks, temporary holding zones, storage racks, and dispatch areas. When workers record each transfer manually, missed scans can create gaps in inventory records. RFID identification offers another way to capture pallet movements at suitable monitoring points.

Active RFID tags contain a power source that supports signal transmission. This differs from passive tags, which rely on energy from a reader to respond. The active design can support identification over greater distances, depending on the tag, reader, environment, and system configuration.

Warehouse operators can attach suitable tags to reusable pallets and configure readers around key movement routes. The collected data can help staff identify pallet locations and review movement histories. Physical placement still matters because metal structures, stored goods, and the warehouse layout can affect radio performance.


Improving Visibility at Receiving and Dispatch

Receiving and dispatch areas often experience concentrated movement during busy periods. Workers need to confirm incoming goods, stage outgoing orders, and identify pallets awaiting inspection. Repeated manual checks can add work when several vehicles arrive within a short period.

Long range active RFID tags can support identification at selected checkpoints when compatible readers are installed. Instead of requiring staff to scan every tagged item individually, a configured system may detect tagged assets as they pass through monitored areas. The actual results depend on read-zone design and the handling process.

Businesses should test the system using real pallet loads and normal traffic patterns. Testing can reveal whether nearby storage zones create unwanted reads or whether reader placement leaves gaps. These findings help technical teams adjust the installation before expanding it across the facility.


Locating Tools and Reusable Equipment

Warehouse operations depend on more than inventory. Handheld equipment, maintenance tools, lifting accessories, and reusable containers may move between teams throughout the day. When these assets lack clear location records, employees can spend time searching for them or arranging replacements.

An active identification system can associate each tagged asset with a unique record. Readers placed at selected entrances or work zones can help establish where an item was last detected. This approach is useful when equipment circulates through a large site and individual scans are difficult to maintain.

However, identification data does not automatically provide continuous indoor positioning. A detection event shows that a tag was read within a configured area. Businesses should distinguish checkpoint-based tracking from systems designed to calculate more precise locations, especially when setting expectations for staff.


Managing Outdoor Storage and Yard Transfers

Some warehouses use outdoor yards for pallet staging, container handling, or temporary asset storage. Rain, dust, and temperature changes can complicate the use of identification devices in these areas. Equipment selection should account for the conditions where tags will operate.

For outdoor applications, active RFID tags with suitable environmental protection can help businesses identify pallets and other tagged assets. An IP rating is particularly relevant when equipment may encounter water or dust. Buyers should also check mounting methods and confirm that the selected tag suits the asset’s surface.

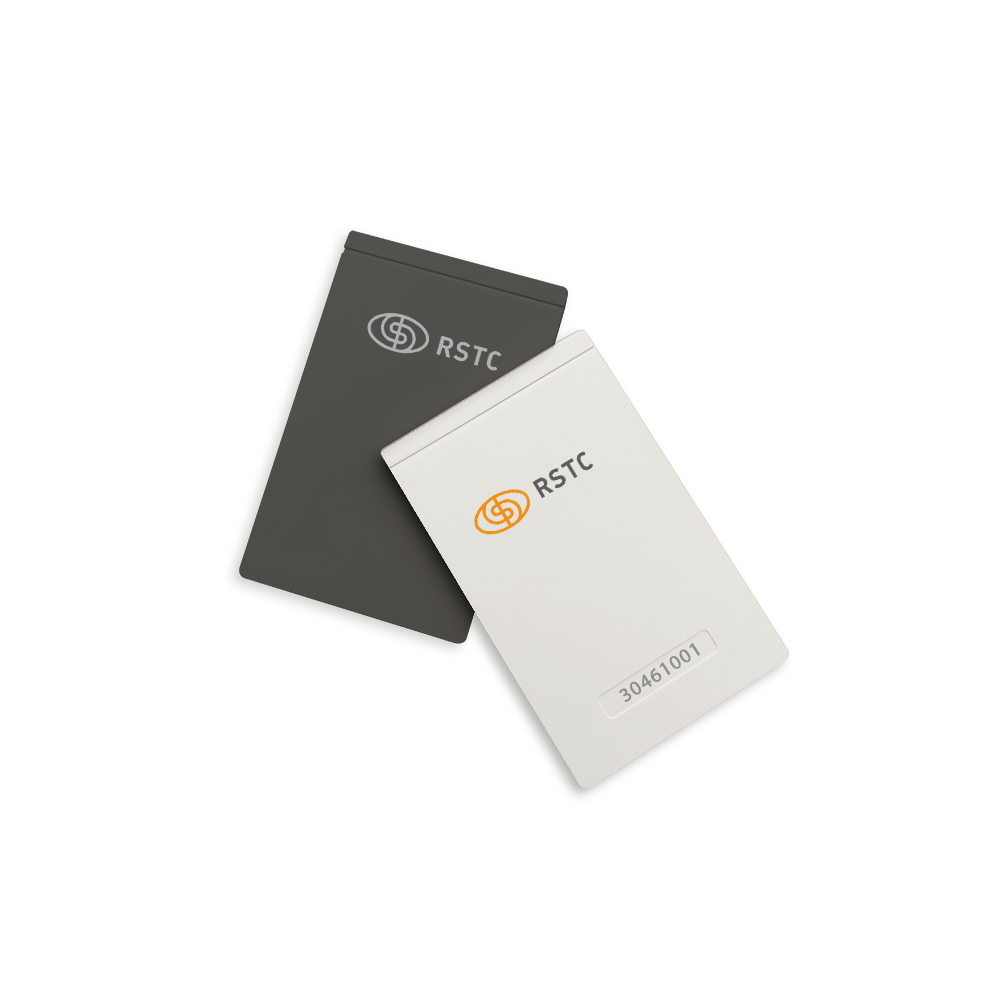
RSTC offers the RS-AT04 Rugged 2.45GHz Active RFID Card for applications such as pallet tracking, boat management, asset tracking, and tooling identification. Its IP67 waterproof design supports use in demanding environments, while its operating frequency falls within the 2.4–2.48 GHz ISM band.


Choosing a Suitable Read Range

Read distance is an important factor when designing a warehouse identification system. Shorter distances may suit controlled workstations, while wider coverage can be useful around yard entrances, loading zones, and open storage areas. Selecting equipment based on distance alone, however, can lead to poor results.

The RS-AT04 supports an adjustable reading distance of up to approximately 120 meters in an open environment, with actual performance depending on the reader, tag settings, antenna configuration, and deployment conditions. This figure provides a reference for planning, rather than a guarantee of the same performance in every warehouse. Building materials, tag orientation, interference, and reader configuration can influence actual detection.

When evaluating long range active RFID tags, warehouse teams should run tests at representative distances and with typical loads. They should also check for overlapping read zones and unwanted detections from neighboring areas. These checks help determine whether the proposed layout supports the intended workflow.


Planning Battery Life and Maintenance

Battery performance affects maintenance schedules and the reliability of long-term asset tracking. If tags stop transmitting unexpectedly, the system may lose visibility of the associated assets. Warehouse managers should therefore consider battery status alongside identification range and environmental protection.

The RS-AT04 features a low-battery alarm and a battery design intended to support low power consumption, high capacity, and a wide operating temperature tolerance. These features can help maintenance teams identify tags that may need attention. Buyers should confirm the expected service interval with the supplier for their intended operating conditions.

RSTC provides an option for businesses assessing active identification in warehouse and outdoor asset-management workflows. Before deployment, procurement and engineering teams should confirm reader compatibility, installation requirements, tag attachment, and integration with existing inventory software. A pilot project can reveal practical issues before the system is expanded. For more guidance on planning read zones, testing RFID performance, and connecting RFID data with warehouse workflows, see RSTC’s RFID warehouse management system deployment guide.


Make the Technology Fit the Workflow

The practical uses of RFID in warehouse management include pallet tracking, receiving and dispatch monitoring, reusable equipment identification, and outdoor asset management. The right setup depends on movement patterns, required read distances, environmental conditions, and the accuracy expected from location records.

Businesses evaluating active RFID tags should begin with a defined operational problem and test the proposed system under real working conditions. With suitable planning, RSTC and its RS-AT04 card can be considered as part of an identification approach for facilities that need wider-area detection and water-resistant hardware.


November 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

From 3D Reconstruction to Decisions: How Spatial AI Streamlines Geospatial Workflows

by addlinkspot November 10, 2026
written by addlinkspot

Spatial data has become an important resource for infrastructure management, public safety, surveying, and low-altitude operations. Yet collecting aerial imagery and geographic information is only the first step. Organizations must also reconstruct environments, identify relevant objects, interpret spatial relationships, and turn analysis results into practical decisions. Spatial artificial intelligence (AI) brings these stages closer together, helping professional teams organize complex geospatial workflows and make better use of the information they collect.


Building a Reliable Foundation with 3D Reconstruction


The workflow begins with collecting suitable spatial data. Unmanned aerial vehicles (UAVs), cameras, and other surveying equipment can capture overlapping images of buildings, terrain, transport networks, and industrial sites. Photogrammetry uses image relationships to derive three-dimensional information, provided that image coverage, camera characteristics, positioning data, and processing quality are appropriate. The U.S. Geological Survey documents how photogrammetric methods can generate point clouds, elevation models, and orthomosaics from aerial imagery.


AI 3D reconstruction extends this foundation by combining computer vision and reconstruction techniques to create digital representations of physical environments. Depending on the data and method, outputs may include textured 3D meshes, point clouds, and orthomosaics. These formats serve different purposes: meshes represent surface geometry, point clouds preserve spatial measurements, and orthomosaics provide geometrically corrected aerial views.


However, reconstruction quality depends on more than the processing algorithm. Image overlap, lighting, surface texture, positioning accuracy, and occlusion can affect the results. Professional teams should establish data-quality criteria before collection and validate reconstructed outputs against project requirements.


Connecting Spatial Intelligence Solutions Across the Workflow


Once spatial data has been reconstructed, the next task is to extract information that supports a defined operational objective. Traditional workflows may require staff to switch between mapping software, image viewers, spreadsheets, and reporting tools. Each handoff can introduce delays, duplicated work, or inconsistencies between datasets.


Well-designed spatial intelligence solutions connect data preparation, reconstruction, AI-based interpretation, and the delivery of analytical results. Rather than treating a 3D model as the final deliverable, teams can use it as a foundation for identifying objects, locating features, and examining their spatial relationships.


This integration does not eliminate the need for professional review. Different projects require different coordinate systems, classification rules, accuracy thresholds, and output formats. Clear interfaces between workflow stages help teams identify where data originates, how it has been processed, and whether the resulting information is suitable for its intended use.


Turning Visual Information into Measurable Findings


Computer vision helps convert large image collections into structured information. Depending on the model and task, AI can classify image content, detect specified objects, or assign semantic labels to individual pixels. Geospatial platforms can then represent findings as mapped features for further analysis. Esri’s documentation describes these techniques and their application to imagery-based GIS workflows.


For infrastructure managers, this process may help identify visible assets or locate features requiring closer inspection. Emergency response teams may use mapped objects and reconstructed terrain to improve their understanding of an incident area. Surveying professionals can compare spatial outputs with existing records to investigate discrepancies.


AI 3D reconstruction becomes more useful when its outputs are linked to relevant attributes and geographic coordinates. A detected object is more actionable when analysts can determine where it is, what category it belongs to, and how it relates to surrounding structures. Confidence scores and human verification can also help teams evaluate uncertain results before operational use.


From Analysis Results to Operational Decisions


The value of spatial AI depends on how effectively its outputs support real decisions. A detection result alone may not tell an asset manager whether a site needs further inspection. Teams must interpret findings alongside project records, operating procedures, environmental conditions, and other relevant evidence.


Spatial intelligence solutions can support this process by organizing mapped features, measurements, and visual context into outputs that decision-makers can review. For example, infrastructure teams may prioritize field inspections based on the location and condition of visible assets. Emergency planners may combine reconstructed scenes with incident information to assess access routes and identify areas requiring attention.


The final decision should remain tied to the reliability of the underlying evidence. Analysts need to understand model limitations, review ambiguous findings, and distinguish observed conditions from AI-generated interpretations. This approach makes spatial analysis more practical without treating algorithmic results as definitive judgments.


Applying End-to-End Spatial AI in Professional Environments


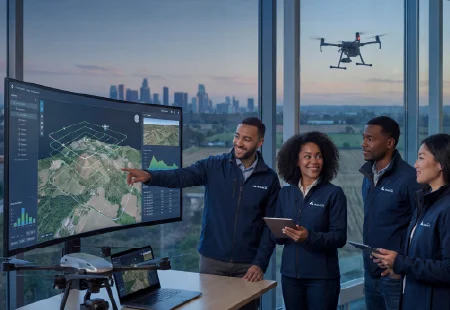
Integrating collection, reconstruction, and analysis is particularly relevant when organizations manage large areas or time-sensitive operations. At Icecypress Technology, the technology portfolio spans 3D reconstruction, UAV mapping, and spatial AI, with applications in infrastructure, mapping, inspection, and emergency response. Its DroneSwarm system focuses on onboard analysis and multi-UAV collaboration, while TrackSight supports target tracking and analytics.


These capabilities illustrate how AI 3D reconstruction can fit into a broader operational process rather than functioning as an isolated modeling task. The appropriate configuration depends on the mission, available equipment, data volume, communications conditions, and required deliverables.


For B2B buyers, evaluating a platform therefore involves more than comparing model detail or processing speed. Procurement teams should examine supported data formats, integration requirements, deployment environments, validation procedures, and the level of technical support available. Pilot projects can help establish whether the workflow meets operational and regulatory needs before wider implementation.


Building a More Connected Decision-Making Process


Spatial AI is most valuable when it connects reliable data collection with meaningful interpretation and practical action. By combining photogrammetry, 3D modeling, computer vision, and geospatial analysis, organizations can reduce fragmented processing and create a clearer path from raw imagery to decision-ready information.


For companies exploring spatial intelligence solutions, the priority should be a workflow that fits their actual operational requirements, with transparent data quality checks and appropriate human oversight. Icecypress Technology‘s work across reconstruction, UAV mapping, and spatial analysis provides one example of this integrated approach. The long-term objective is not simply to produce richer visual models, but to make spatial information more useful for professional planning, inspection, and response.


November 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

Mitigating Financial Risks Using Revenue Assurance Telecom Software Solutions

by addlinkspot November 10, 2026
written by addlinkspot

Revenue leakage can quietly weaken a telecom operator’s financial performance, even when subscriber numbers and service usage appear healthy. Unbilled calls, inaccurate charging rules, delayed settlements, and inconsistent records between network and billing systems may create discrepancies that remain unnoticed for months.


Effective revenue assurance helps operators identify these gaps, investigate their causes, and protect income without relying solely on end-of-month financial reports. As telecom services become more complex, telecom software solutions can support better data visibility and more disciplined revenue controls.


Understanding the Main Sources of Telecom Revenue Leakage

Telecom revenue leakage often originates from differences between service delivery and financial records. A network may record a completed transaction while the billing platform fails to generate the corresponding charge. Similar discrepancies can arise when tariff plans change, roaming agreements are updated, or promotional discounts are configured incorrectly. These issues may affect individual transactions or accumulate across millions of records, making manual inspection increasingly impractical.


Another challenge comes from the growing variety of services offered by operators. Mobile connectivity, fixed broadband, cloud services, and digital subscriptions may use different charging mechanisms and accounting processes. Without consistent reconciliation, an operator can struggle to determine whether a discrepancy reflects legitimate commercial activity, a configuration error, or an actual loss of revenue. Effective revenue assurance establishes controls across these interconnected processes instead of examining billing outcomes in isolation.


The financial impact extends beyond missed charges. Incorrect invoices can trigger customer disputes, increase support workloads, and delay payments. Unresolved settlement differences may also complicate relationships with roaming partners, resellers, and other service providers. Operators benefit from classifying discrepancies by financial exposure, frequency, and operational cause, allowing investigation teams to prioritize issues that could materially affect cash flow or financial reporting.


Building Reliable Controls Across Telecom Systems

A dependable control framework connects records from network elements, mediation platforms, charging engines, billing applications, and financial systems. Each source captures a different stage of the commercial process, so comparisons must account for transaction identifiers, timestamps, service categories, and applicable pricing rules. Consistent data definitions make it easier to identify missing records, duplicate events, and differences between measured usage and billed amounts.


Automation can strengthen these checks by processing large datasets according to predefined business rules. Telecom software solutions can help organize reconciliation workflows, flag unusual transaction patterns, and direct exceptions to the appropriate operational teams. Automated checks are especially useful for recurring discrepancies, while human review remains important for ambiguous cases involving contractual terms, exceptional adjustments, or legitimate billing variations.


Control design also requires clear ownership. Network operations may investigate missing usage records, billing teams may review charging configurations, and finance departments may validate settlement differences. Shared case records, documented escalation paths, and consistent resolution deadlines reduce the risk of the same issue being investigated repeatedly. A well-governed revenue assurance process records not only the amount recovered or corrected but also the underlying cause, the responsible system, and the action needed to prevent recurrence.


Applying Analytics to Detect Financial Anomalies

Rules-based monitoring can identify familiar problems, but statistical analysis helps reveal irregularities that fixed thresholds may miss. Unusual changes in average revenue per user, transaction volumes, discount rates, or service activation patterns can indicate emerging weaknesses. Analysts should compare these indicators with historical baselines and relevant business conditions before deciding whether an anomaly requires intervention.


Useful monitoring depends on selecting meaningful metrics. Operators can track the value of unresolved discrepancies, the time required to investigate them, the proportion of exceptions successfully resolved, and the recurrence rate of previously identified problems. These measures make revenue assurance more actionable by connecting technical findings with financial outcomes rather than treating every alert as equally important.


Data quality remains a critical consideration. Missing fields, inconsistent timestamps, delayed data feeds, and changes to system interfaces can produce misleading alerts. Telecom software solutions should support traceable data transformations and clear exception reporting so analysts can distinguish genuine financial exposure from errors introduced during processing.


Regular rule reviews are equally important as new tariffs, products, and partner agreements change the expected behavior of transactions. Whale Cloud’s telecom software solutions are designed to support these traceable data pipelines and actionable analytics workflows.


Strengthening Governance and Long-Term Risk Management

Technology alone cannot address every source of financial risk. Operators need documented control procedures, clear accountability, and cooperation between commercial, technical, and finance teams. Periodic reviews of pricing changes, product launches, partner contracts, and system integrations help identify weaknesses before they affect large transaction volumes. Audit trails also make it easier to explain why adjustments occurred and how discrepancies were resolved.


Risk assessments should reflect both the probability and potential impact of a problem. A small recurring error across a high-volume service may create greater exposure than a larger isolated discrepancy. Telecom software solutions can help teams categorize exceptions, maintain investigation histories, and monitor corrective actions. However, automated findings still require appropriate validation, access controls, and oversight to prevent inaccurate adjustments or unnecessary customer charges.


For operators evaluating digital transformation initiatives, Whale Cloud offers a broader telecommunications technology context in which billing processes, data management, and operational intelligence can be considered together. Its portfolio includes Digital BSS, which is relevant to business support processes. Any implementation should be assessed against the operator’s existing architecture, integration requirements, governance arrangements, and measurable business objectives rather than technology claims alone.


Turning Financial Visibility Into Sustainable Control

Financial protection becomes more effective when monitoring, investigation, and prevention operate as a continuous cycle. Operators that document recurring issues can identify systemic weaknesses, refine control rules, and assess whether corrective actions deliver lasting improvements. This approach also supports more informed decisions about technology investment, operational staffing, and the allocation of audit resources.


Long-term progress depends on measurable results, reliable evidence, and collaboration across departments. By combining disciplined revenue assurance practices with appropriate telecom software solutions, operators can improve the visibility of financial discrepancies and respond to risks with greater consistency. Whale Cloud provides relevant technology capabilities for telecommunications digitalization, while each operator must determine the controls, integrations, and governance model suited to its own business environment.


November 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

How Does CMM Laser Scanning Reduce Inspection Time and Rework Costs?

by addlinkspot November 10, 2026
written by addlinkspot

Manufacturers face constant pressure to maintain dimensional accuracy while shortening production cycles and controlling quality-related expenses. Traditional inspection methods can become time-consuming when components have complex contours, multiple measurement points, or difficult-to-reach surfaces. Modern optical metrology offers another approach by capturing extensive three-dimensional data for comparison with design specifications.


Understanding how a CMM laser scanner improves inspection efficiency helps manufacturers identify opportunities to reduce delays, detect defects earlier, and limit unnecessary rework.


Capturing More Dimensional Data in Less Time


Contact measurement relies on a probe touching individual points to establish dimensions. Although this method remains effective for many applications, inspecting complex surfaces may require numerous measurements and repeated repositioning. Laser scanning captures dense point-cloud data across a surface, allowing inspectors to evaluate more geometric details within a single scanning process.


This broader data collection can reduce manual measurement steps and accelerate the inspection of freeform surfaces, molded components, and intricate machined parts. The resulting data also supports dimensional comparisons beyond a limited set of predetermined points, helping quality teams identify deviations that conventional sampling might overlook.


Identifying Defects Before They Become Expensive


Rework costs often increase when dimensional problems remain undetected until assembly or final inspection. A component with an incorrect contour, misplaced feature, or unexpected deformation may require additional machining, adjustment, or replacement. If the defect affects subsequent operations, the financial impact can extend across labor, materials, machine time, and delivery schedules.


Integrating scanning into in-process quality checks helps manufacturers identify discrepancies earlier. By comparing measured geometry with CAD data, engineers can investigate deviations before additional production resources are committed. This approach does not eliminate every defect, but it provides more information for timely corrective action and more consistent process control.


Improving Inspection of Complex Workpieces


Large, irregular, or contoured components present practical challenges for conventional probing. Inspectors may need to change probe orientations, reposition equipment, or measure many individual locations to assess the geometry adequately. These steps add handling time and can make inspection procedures more demanding.


A portable measuring arm equipped with a laser scanning head provides greater flexibility for inspecting complex workpieces on the shop floor. Non-contact scanning can also benefit delicate surfaces that could be affected by probe contact, provided the material and surface finish are suitable for the optical system. Broader surface coverage helps engineers evaluate geometric variation with less dependence on individual point measurements.


Reducing Setup and Operator Workload


Inspection time includes more than data acquisition. Equipment setup, workpiece repositioning, access to hidden features, and operator fatigue can all influence the total time required to complete a measurement task. A practical inspection system should therefore improve both measurement coverage and ease of operation.


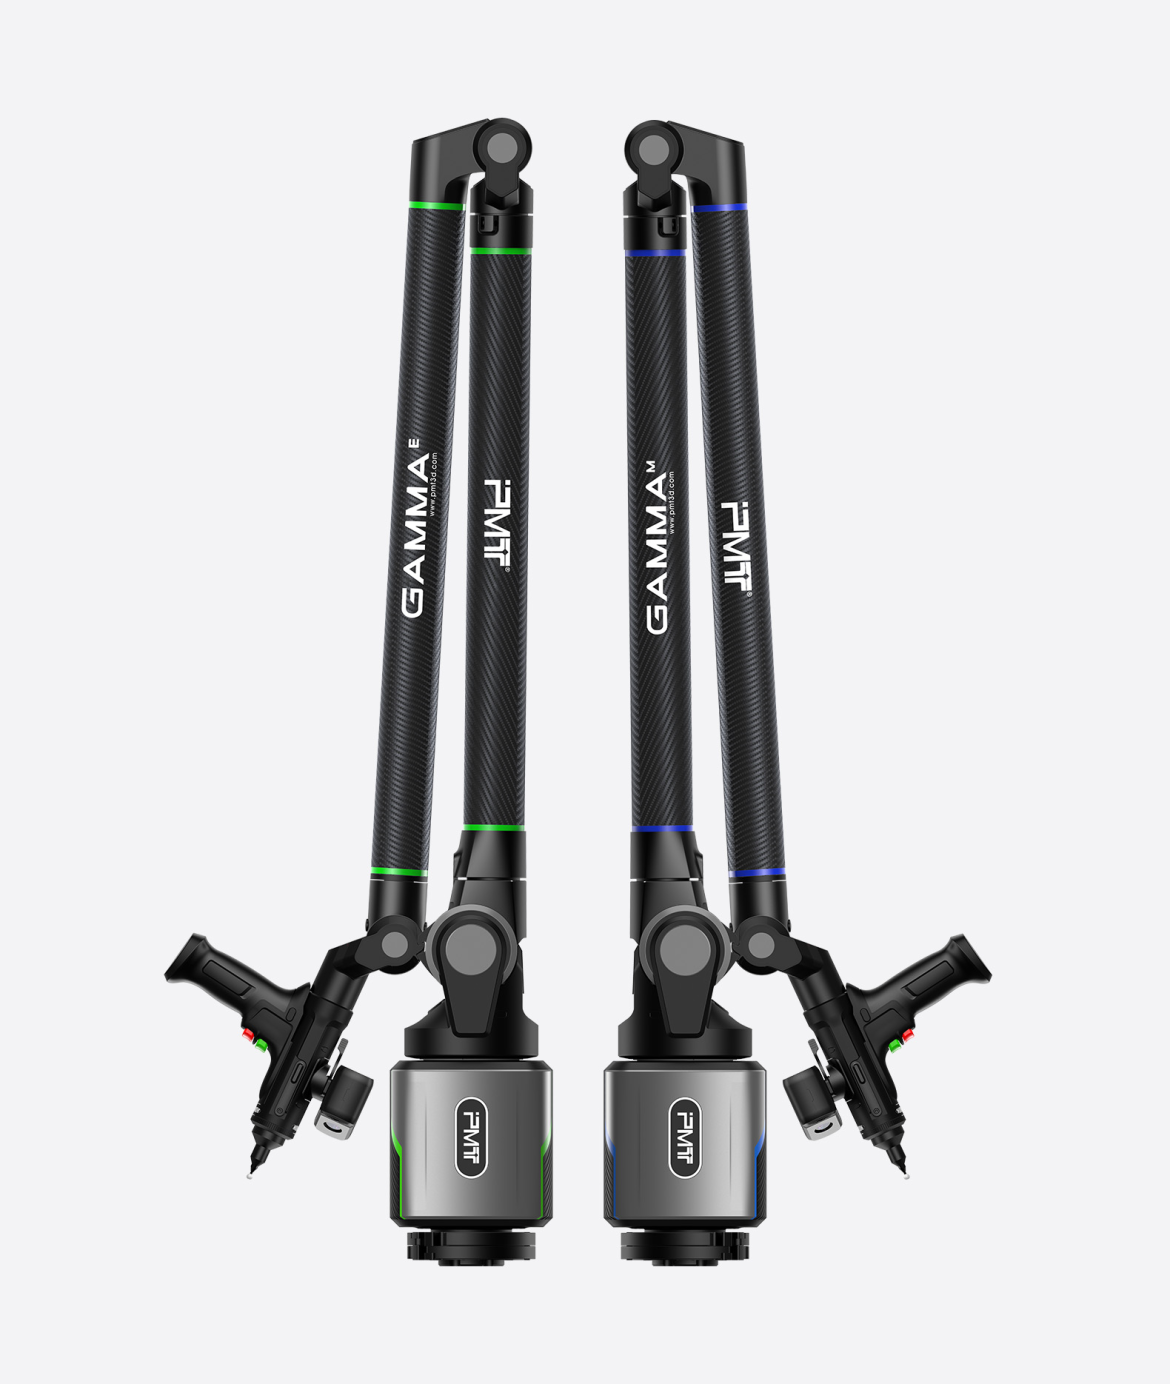
The PMT GAMMA 7/8-AXIS+GH/GS Series combines a portable measuring arm with a blue-light scanning head. Its optimized optical design supports stable scanning accuracy, while adjustable laser brightness allows operators to reduce eye fatigue. The balancing mechanism reduces joint loading and supports flexible handling, helping make repeated inspection tasks more manageable.


Simplifying Access and Data Processing


Repeatedly moving equipment around a component can increase measurement time and introduce additional opportunities for positioning errors. A compatible rotary worktable can help address this challenge by allowing the workpiece to rotate while the equipment remains in a stable position.


PMT’s GAMMA platform supports an eight-axis rotary worktable configuration. This arrangement can reduce the need to reposition the measuring arm or workpiece to reach different areas. Fewer scanning setups may also simplify alignment and subsequent data processing, although the actual time savings depend on component geometry, fixture design, and inspection requirements.


A CMM laser scanner can further support efficient reporting when its measurement data is integrated with suitable inspection software. Comparing a point cloud with the nominal CAD model helps visualize dimensional deviations and document results. Clear deviation maps and inspection reports make it easier for quality engineers to communicate findings and determine whether a component requires correction.


Evaluating the Return on Investment


The financial benefit of faster inspection depends on more than scanning speed. Manufacturers should assess the complete inspection cycle, including setup, acquisition, data processing, reporting, and any additional verification. They should also consider the costs associated with scrap, rework labor, delayed deliveries, and downstream assembly problems.


A useful evaluation compares the original inspection process with the proposed scanning workflow across representative parts. Relevant measures include inspection time per component, defects detected before assembly, repeat inspection frequency, and total rework expenditure. Accuracy, repeatability, calibration, operator training, and environmental conditions must also be considered to ensure that faster measurement still meets the required quality standards.


The most effective investment is one that delivers measurable improvements under actual production conditions rather than relying solely on advertised scanning speeds.


Building a More Efficient Quality Inspection Process


Laser scanning can help manufacturers shorten dimensional inspection, capture complex geometry, and identify deviations earlier in production. When combined with appropriate analysis software and a well-designed quality workflow, these capabilities can reduce avoidable rework and improve manufacturing consistency.


For companies evaluating portable metrology, PMT‘s GAMMA series CMM laser scanner offers a combination of blue-light scanning, ergonomic arm design, and optional rotary-table integration. Selecting the right configuration requires matching its performance to component geometry, tolerance requirements, and inspection objectives. With a validated process, manufacturers can make quality decisions sooner while maintaining the accuracy and traceability their operations demand.

November 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
  • 1
  • 2
  • 3
  • …
  • 65

Recent Posts

  • Water Play Structure Spare Parts and Service Life Planning
  • How Can Dispensing Process Data Improve Production Traceability?
  • Portable Multi Gas Detectors: How Channels Share One Pump
  • Quality Tests Used by Car Starting Battery Manufacturers
  • What Are the Best Uses for Long Range Active RFID Tags in Modern Warehouse Management?

Recent comments

No comments to show.

About Me

About Me

Freelance Developer

My name is Brian, freelance developer based in London, UK. Welcome to my internet journal where I started my learning journey.

Keep in touch

Facebook Twitter Linkedin Youtube Github

Resources

  • Water Play Structure Spare Parts and Service Life Planning

    November 22, 2026
  • How Can Dispensing Process Data Improve Production Traceability?

    November 22, 2026
  • Portable Multi Gas Detectors: How Channels Share One Pump

    November 20, 2026

Recent Posts

  • Water Play Structure Spare Parts and Service Life Planning

    November 22, 2026
  • How Can Dispensing Process Data Improve Production Traceability?

    November 22, 2026
  • Portable Multi Gas Detectors: How Channels Share One Pump

    November 20, 2026
  • Quality Tests Used by Car Starting Battery Manufacturers

    November 17, 2026
  • What Are the Best Uses for Long Range Active RFID Tags in Modern Warehouse Management?

    November 13, 2026

Categories

  • 3D Sacnner (1)
  • Agriculture (1)
  • Automobile (2)
  • Biology (4)
  • Business (109)
  • Car (1)
  • Catalyst (1)
  • Coding (18)
    • Backend (6)
    • Frontend (6)
    • Guide (6)
  • Dentistry (1)
  • Dress (1)
  • Economy (30)
  • Furniture (4)
  • Global Trade (33)
  • Healthcare (1)
  • Industry (153)
  • Innovation (81)
  • Jewelry (3)
  • Kitchen (2)
  • knife (1)
  • LED (2)
  • light (1)
  • Living (1)
  • m (1)
  • Machine (16)
  • Manufacturer (51)
  • Market (32)
  • Medical (14)
  • News (58)
  • Online (1)
  • Product (12)
  • Resources (6)
  • Smart Lock (1)
  • Tech (67)
  • Technology (20)
  • Vegetables indoor (1)

Backend

  • Water Play Structure Spare Parts and Service Life Planning

    November 22, 2026
  • How Can Dispensing Process Data Improve Production Traceability?

    November 22, 2026
  • Portable Multi Gas Detectors: How Channels Share One Pump

    November 20, 2026
  • Quality Tests Used by Car Starting Battery Manufacturers

    November 17, 2026

Frontend

  • Water Play Structure Spare Parts and Service Life Planning

    November 22, 2026
  • How Can Dispensing Process Data Improve Production Traceability?

    November 22, 2026
  • Portable Multi Gas Detectors: How Channels Share One Pump

    November 20, 2026
  • Quality Tests Used by Car Starting Battery Manufacturers

    November 17, 2026

Guide

  • Getting Started with Backend Development 101

    January 25, 2019
  • The Skills You Need to Be a Back-End Developer

    January 25, 2019
  • Modern Backend Developer in 2019

    January 25, 2019
  • Integrating with an API Backend

    January 25, 2019
  • Facebook
  • Twitter
  • Linkedin
  • Youtube
  • Email
  • Github
  • Stack-overflow

All Right Reserved. Designed and Developed by addlinkspot.

addlinkspot
  • Home
  • Resources
  • Frontend
  • Guide
  • Backend